






Complex-Shape Tube Bending Machine
Complex-Shape Tube Bending Machine
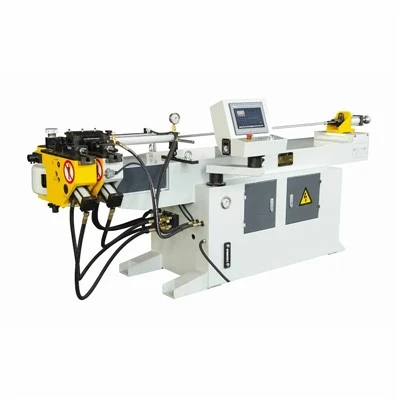
The multi-axis complex-shape tube bending machine executes spatial, multi-plane, and variable-radius transformations on metallic tubing without secondary welding or forming. Built on a rigid, finite-element-analyzed (FEA) cast-iron bed, the platform integrates multi-axis servo control for feeding, rotation, and bending.
Engineering focus centers on maintaining cross-sectional integrity across tight center-line radii (CLR <= 1.5D). The integrated CNC architecture processes native CAD files (STEP/IGES/XT) to auto-calculate springback compensation, eliminating iterative trial-and-error programming for high-mix, low-volume production environments as well as automated, continuous production lines.
Technical Specifications
|
Specification Item |
Industrial Standard Parameters |
Heavy-Duty Variant |
|
Max. Tube Outer Diameter (OD) |
Φ 16 mm - Φ 50 mm |
Φ 51 mm - Φ 114 mm |
|
Max. Wall Thickness |
3.0 mm (Mild Steel) |
6.0 mm (Mild Steel) |
|
Min. Center Line Radius (CLR) |
1.0D - 1.5D |
1.2D - 2.0D |
|
Max. Bending Angle |
190° |
190° |
|
Bending Axis Precision |
± 0.05° |
± 0.03° |
|
Feeding Axis Precision |
± 0.05 mm |
± 0.03 mm |
|
Rotation Axis Precision |
± 0.05° |
± 0.03° |
|
Controlled Axes (CNC) |
5-Axis (Feed, Rotate, Bend, Carriage Side-Shift, Mandrel Shift) |
7-Axis (Includes Booster & Wiper Die Positioning) |
|
Drive System |
Absolute-Encoder AC Servos |
Direct-Drive Torque Motors + Absolute Servos |
|
Hydraulic System Pressure |
14 MPa |
21 MPa with proportional flow control |
|
Software Compatibility |
SolidWorks, CATIA, Inventor (STEP/IGES/XT direct import) |
SolidWorks, CATIA, Inventor (STEP/IGES/XT direct import) |
Key Features
Real-Time Springback Compensation: Algorithms measure material tensile variations across batches and dynamically adjust bend angles to eliminate trial scrap.
Synchronized Booster Carriage: Applies axial pushing force during bending to neutralize wall thinning on the outer radius of tight CLR bends.
Multi-Stack Tooling Stack: Accommodates up to three different radii or fixed/rotary combinations on a single tooling stack to process complex geometries without manual tool swaps.
Collision Detection Simulation: 3D graphical programming software simulates the entire bending sequence against machine kinematics before physical execution.
Direct CAD Import Interface: Accepts direct file ingestion of 3D tube center-line data (compatible with SolidWorks, CATIA, and Inventor), translating spatial coordinates directly into machine G-code.
Working Process
Material Loading: The raw tube stock is loaded onto the pneumatic feeding carriage, secured by a self-centering hydraulic collet.
Spatial Positioning: The feeding axis advances the tube to the precise longitudinal position (Y-axis), while the rotation axis rotates the tube to the specified spatial plane (B-axis).
Mandrel & Wiper Positioning: The internal mandrel extends inside the tube throat to support internal wall structure, and the wiper die locks tight against the tangent point to prevent outer-radius wrinkling.
Bending Execution: The pressure die and clamp die secure the tube against the bend die. The main bend arm rotates to the programmed angle (C-axis) under closed-loop servo control.
Extraction & Release: The mandrel retracts fractionally before the clamp and pressure dies open, clearing the formed component for the next bend cycle or final unloading.
Tooling & Configuration
Successful complex tube bending relies entirely on correct tooling geometry matching the material's elongation and yield strength.
Bend Die & Clamp Die: Match the exact tube outer diameter and profile (round, square, or oval) to distribute clamping force without surface marring.
Pressure Die: Synchronized with the bend die speed to push material through the radius zone, minimizing outer wall thinning.
Wiper Die: Positioned immediately ahead of the bend point; manufactured from aluminum bronze or Ampco metal to eliminate galling on stainless steel or titanium tubes.
Mandrel Assemblies: Configured as plug mandrels, formed ball mandrels (single, double, or multi-ball), or flexible link mandrels depending on the CLR severity and tube wall thickness.
Customization
Extended Bed Lengths: Tailored carriage travel lengths from 3,000 mm up to 12,000 mm to accommodate extra-long structural tubular parts.
Automated Loading/Unloading Integration: Interfacing capability with industrial gantry loaders, robotic arms, or bundle magazine loaders for lights-out manufacturing cells.
Punching & Cutting Integration: Inline hydraulic punching modules integrated prior to or after the bending sequence for multi-operation manufacturing cells.
Specialized Control Integration: Custom PLC interfaces (Siemens, Mitsubishi, or Beckhoff) mapped to specific factory SCADA or MES execution networks.
Quality & Testing
Structural stability and long-term geometric repeatability originate from controlled machining processes and rigorous verification protocols.
Bed Annealing & Machining: Machine weldments undergo thermal stress relief annealing to eliminate residual welding stress, followed by precision milling on large CNC gantry machining centers in a temperature-controlled environment.
Geometric Calibration: Laser interferometer tracking verifies multi-axis positioning accuracy, repeatability, and squareness prior to assembly.
Factory Acceptance Testing (FAT): Each machine undergoes an endurance test running a minimum of 500 consecutive test cycles using customer-supplied raw material samples, verifying dimension reports via 3D optical scanning or CMM inspection.
fAQ
Q: How does the machine compensate for material batch springback variations?
A: The control system integrates an integrated springback database coupled with closed-loop angular feedback encoders. When material yield strength fluctuates between batches, the machine performs a test bend on the initial piece, measures the actual angular recovery via optical feedback, and automatically recalculates the over-bend angle for subsequent cycles.
Q: What is the minimum centerline radius (CLR) achievable without a mandrel?
A: For standard carbon steel tubes with a wall thickness ratio (D/t) greater than 25, a mandrel-less bend is achievable at CLR = 3D. For tight configurations (CLR <= 2D) or thin-walled applications, a multi-ball mandrel and wiper die are required to prevent ovality and collapse.
Q: Can the machine process non-round tubes, such as rectangular or oval profiles?
A: Yes. By replacing the standard round tooling stack with profile-specific matched tooling sets (including specialized wiper dies and shape-matched mandrels), the machine processes square, rectangular, D-shape, and asymmetric oval sections while maintaining twist and profile control.
Q: What file formats are compatible with the CNC control software?
A: The system directly imports 3D CAD files in STEP, IGES, and XT formats from design software like SolidWorks, CATIA, and Inventor. The built-in parser automatically extracts center-line radius, straight lengths, and rotation angles, converting spatial geometry into executable machine code without manual coordinate entry.
Q: What is the standard tooling changeover time?
A: The machine features a quick-change tooling design utilizing hydraulic or manual quick-release clamp pins. A full tooling stack changeover (bend die, clamp die, pressure die, and wiper holder) takes between 20 to 30 minutes, depending on the machine model size.
Q: What utility requirements are needed for installation?
A: Standard operation requires a 3-phase electrical supply (typically 380V/480V, 50/60Hz, sized between 25 kVA and 45 kVA depending on servo sizing) and a stable compressed air supply at 0.6 MPa to 0.8 MPa for pneumatic clamping and lubrication actuators.
Hot Tags: complex-shape tube bending machine, China complex-shape tube bending machine manufacturers, suppliers, factory, Automatic Hydraulic Tube Bending Machine, CNC Automatic Pipe Bending System, CNC Copper Pipe Bending Machine, Hydraulic Stainless Steel Tube Bending Machine, Rectangular Metal Pipe Cutting Machine, Square Tube Sawing Machine
You Might Also Like




Send Inquiry