






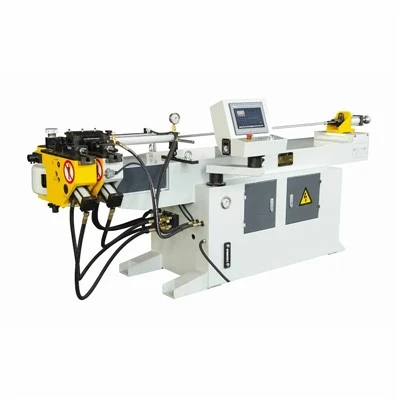
Multi-Radius Aluminum Tube Bending Machine
Multi-Radius Aluminum Tube Bending Machine
Engineered for thin-wall aluminum fabrication, this multi-radius bending machine integrates programmable multi-axis motion to execute consecutive different radii on a single tube without manual repositioning. Built on a heavy-gauge stress-relieved steel frame, it eliminates torsional deflection during high-speed pushes. The system features a synchronized hydraulic-electric hybrid drive, delivering repeatable precision for high-volume automotive and HVAC production lines.
Technical Specifications
|
Specification Parameter |
Value / Range |
|
Max. Tube Diameter |
OD 6mm - 76mm |
|
Max. Wall Thickness |
0.5mm - 4.0mm (Aluminium alloys: 6061, 3003, 5083) |
|
Min. Centerline Radius (CLR) |
1.0 x OD (Dependent on tooling and wall thickness) |
|
Max. Bending Angle |
180 deg + Springback Compensation |
|
Bending Axis Precision |
+/- 0.05 deg |
|
Feeding & Rotation Precision |
+/- 0.05mm / +/- 0.05 deg |
|
Control System |
Industrial IPC + Touchscreen NC/CNC Interface |
|
Drive System |
AC Servo Motors + Closed-Loop Hydraulic Boosters |
Key Features
Multi-Radius Stack Tooling: Houses multiple radius dies simultaneously on a shifting stack, allowing automated transitions between tight and wide bends within the same cycle.
Closed-Loop Springback Compensation: Real-time sensor feedback measures aluminum elastic recovery post-bend and dynamically adjusts axis positioning to eliminate trial-and-error scrap.
Programmable Mandrel Extraction: Advanced servo-driven early extraction prevents interior wall wrinkling and cross-section flattening on thin-wall aluminum tubing (OD < 1.5mm).
Fluid-Temperature Thermal Stability: Integrated hydraulic oil cooling prevents viscosity breakdown during 24/7 continuous shift operations.
Working Process
Material Loading: Raw aluminum tube is clamped onto the carriage feed collet; internal mandrel and wiper die are positioned at the tangent point.
Auto-Feeding & Rotation: Servo clamps index the tube longitudinally and rotationally to coordinate the exact spatial angle for the first bend.
Multi-Radius Execution: The pressure die and bend die synchronize pressure while the mandrel stays stationary inside the tube to support the inner wall radius.
Early Extraction & Unclamping: The mandrel retracts fractionally before the bend finishes to prevent tearing, followed by vertical die opening.
Stack Shift & Re-clamping: The tool stack shifts vertically/horizontally to align the secondary radius die for subsequent compound bends without operator intervention.
Applications
EV Thermal Management: Multi-bend aluminum cooling channels routing through battery packs.
HVAC&R Manifolds: Refrigerant distribution headers requiring tight-radius return bends.
Automotive Exhaust & Fluid Lines: Precision structural tubes requiring strict geometric tolerances.
Aerospace Enclosures: Lightweight frame components fabricated from high-strength aluminum alloys.
Tooling & Configuration
Standard Stack Assembly: Comprises bend die, clamp die, pressure die, wiper die, and flexible mandrel balls matched to exact tube OD and wall dimensions.
Material Selection: Tooling machined from Ampco aluminum bronze or hardened tool steel (HRC 58-62) with anti-friction coatings to prevent aluminum galling and scratching.
Quick-Change Interface: Hydraulic quick-release arbors reduce single-stack tooling changeover time to under 15 minutes.
Customization
Tailored Axis Configuration: Expandable from 3 axes (XYZ) to 7 fully interpolated electric axes for complex spatial geometries.
Loading Automation Integration: Compatible with gantry loaders, anthropomorphic robot arms, and pneumatic unloader racks.
Specialized Profiles: Custom die sets engineered for square, rectangular, oval, and specialized extruded aluminum profiles.
Quality & Testing
In-House Machining: Main frames are welded in-house, annealed at 600 deg C to relieve internal welding stress, and finished on CNC floor-boring mills to ensure bed parallelism within 0.02mm/m.
Component Traceability: Critical hydraulic valves and servo drives source exclusively from established industrial brands (Rexroth, Siemens, Yaskawa).
Factory Acceptance Testing (FAT): Every machine undergoes a strict 72-hour continuous dry-run test followed by live material test-bending. Coordinate measuring machine (CMM) inspection reports are verified and archived prior to crating.
FAQ
Q: How does the machine handle springback differences between different aluminum alloy batches like 6061-T6 and 3003-H14?
A: The CNC control system features a material database storing elongation and tensile parameters. Operators input the batch tensile variance, and the system automatically calculates micro-over-bend angles, eliminating manual trial bends.
Q: What prevents aluminum tubing from wrinkling or collapsing on tight inner radii (1.5 x OD)?
A: Wrinkling is prevented through a combination of a multi-ball flexible mandrel, a precisely matched wiper die that hugs the tangent point, and programmable early mandrel extraction driven by high-response servo feedback.
Q: Can a single machine tool stack process both round and square aluminum tubing?
A: No. Bending dies are profile-specific. Switching from round to square tubing requires changing the complete tooling set (bend die, clamp die, pressure die, and mandrel), which takes approximately 20 to 30 minutes.
Q: What are the facility utility requirements for installation?
A: The system requires a standard 3-phase industrial power supply (380V/415V/480V, 50/60Hz), a clean compressed air supply (0.6 MPa), and an ambient operating workshop temperature between 5 deg C and 45 deg C.
Q: What quality inspection reports and compliance documents are provided with shipment?
A: Each shipment includes a CMM dimensional inspection report of test parts, a complete hydraulic/electrical schematic package, ISO9001 quality compliance certificates, and CE conformity documentation.
Q: What is the typical lead time for standard versus customized machine builds?
A: Standard catalog configurations ship within 4 to 6 weeks. Fully custom multi-axis integrations requiring specialized profile tooling validation typically require 10 to 14 weeks from drawing sign-off.
Hot Tags: multi-radius aluminum tube bending machine, China multi-radius aluminum tube bending machine manufacturers, suppliers, factory, Automatic Feeding Tube Sawing Machine, CNC 5 Axis Pipe Bender, CNC Metal Tube Sawing Machine, CNC Thin Wall Pipe Bending Machine, Furniture Pipe Bending Machine, Servo Precision Tube Cutting Machine
Previous
No InformationYou Might Also Like




Send Inquiry